Hey everyone, it’s Jake from [Your Company Name]—today I wanna break down something I get asked about all the time, especially by folks who’re new to using self-tapping inserts: what exactly is the hardness of these things? And no, it’s not just a random number we pull out of thin air for our product specs—this stuff actually matters big time for your project. Let’s cut the jargon, keep it real, and get into it. Self-Tapping Inserts
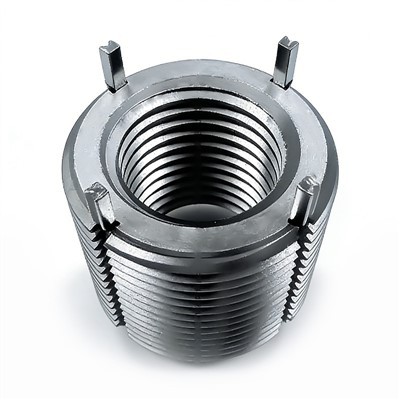
First off, if you’re here because you’ve been struggling with stripped threads in plastic, soft metal, or even thin aluminum parts, you probably already know what self-tapping inserts do. They’re those little threaded liners you twist into a pre-drilled hole, right? Unlike regular inserts that need a pre-threaded hole, these ones carve their own teeth as you drive ‘em in. That’s where the “hardness” part comes in—your insert’s hardness is basically its resistance to being dented, scratched, or deformed when you tap it into a part, or when you tighten a bolt down into it later.
Now, I know when I first started selling these things (back when I was just testing prototypes in my garage, not running a whole team), I confused “hardness” with “strength.” Big mistake. Hardness isn’t about how much weight the insert can hold—that’s tensile strength or load capacity. Hardness is about surface durability and how well the insert maintains its shape during installation and use. Think of it like this: if you have a really hard cookie, it doesn’t bend when you bite it, it crumbles. But if it’s too soft, it squishes. Self-tapping inserts need that sweet spot—hard enough to carve clean threads in the part, but not so hard that it’s brittle and cracks under torque.
Let’s get into the actual numbers, since that’s what most engineers and maintenance guys want. Wait, but hold up—hardness is measured different ways depending on the material, right? For most standard self-tapping inserts we sell, we use two scales: Rockwell C (HRC) for metal inserts and Brinell (HB) for some plastic-compatible ones, but mostly HRC because 90% of our clients are using metal or reinforced plastic parts.
Here’s the lowdown on our product line: our standard carbon steel self-tapping inserts clock in at 35-42 HRC. If you need something heavier duty, our alloy steel ones go up to 48-52 HRC. Wait, but why the range? Because 35 HRC is perfect for thin-gauge aluminum or soft ABS plastic—too hard there, and you’ll crack the base part. The 48-52 HRC is for heavy stuff like thick steel plates, or applications where you’re tightening bolts to 100+ ft-lbs of torque regularly, like industrial machinery or automotive components.
I can hear some of you now: “Jake, why not just make ‘em all 55 HRC so they never fail?” Fair question, but let’s talk about what happens when an insert is too hard. If you crank the HRC above 55, that insert becomes super brittle—like a glass shard. When you go to drive it into a hole, or when a worker over-tightens a bolt, the insert can snap right in half, leaving you with a bigger mess than a stripped thread. I’ve had a client come to me last year with exactly that problem—they bought cheap inserts from a random supplier online that were 58 HRC, and half of them cracked during installation on their drone frames. They switched to ours at 38 HRC, and haven’t had an issue since.
On the flip side, too soft is just as bad. If your insert is under 30 HRC, it’ll deform when you tap it into the part. The little cutting teeth on the insert don’t carve clean grooves—they just push the material out of the way. That means once you tighten a bolt down, the insert will spin, or the threads will strip after a few uses. I had another client a while back who used 28 HRC inserts for their office chair caster mounts. After 6 months of people sitting, rolling, tightening, those inserts had flattened out, and the casters just fell off. Switched to our 36 HRC ones, and that problem’s gone for good.
Wait, let’s make this tangible for anyone who’s not an engineer. Let’s use a common example: mounting a door handle. The door is usually hollow core or soft wood, right? A regular screw would just strip the wood. A self-tapping insert here needs to be hard enough to bite into the wood, but not so hard that you snap it when driving. Our 35 HRC carbon steel inserts work perfect here—enough hardness to carve tight threads in wood, not brittle enough to break if you hit a little knot. Now, if you’re mounting a door to a steel frame, you need something harder—our 45 HRC alloy inserts will carve clean threads in steel, and hold up to the constant opening and closing without deforming.
Another thing people don’t talk about: how the insert’s hardness interacts with the base material’s hardness. If your base part is soft—like zinc die-cast or soft aluminum—your insert needs to be harder than that to carve its own threads. We usually recommend a 10-15 HRC difference between the insert and the base material. So if your aluminum part is 25 HRC, your insert should be 35-40 HRC. If the base is hard steel (40 HRC), go with a 48-50 HRC insert. If you mismatch that? Let’s say you use a 30 HRC insert in 40 HRC steel—those cutting teeth won’t carve anything, they’ll just slide around, and you’ll get a loose insert.
Now, I get that not all projects are the same. That’s why we don’t sell a one-size-fits-all self-tapping insert. We’ve got options for everyone: low-profile inserts for tight spaces, inserts with integrated locking features for vibration-heavy applications (like off-road vehicles), even stainless steel inserts for corrosion-prone environments (those are 32-38 HRC, because stainless steel doesn’t harden as much as carbon steel without getting brittle).
A lot of new customers come to me thinking “higher HRC = better,” and I always have to talk ‘em off that ledge. Hardness is a balance, not a competition. Let’s check a quick real-world example from our own orders: last quarter, we shipped 50,000 inserts to a company making electric bike frames. They initially ordered 52 HRC inserts, but when they tested them, 7% cracked during installation. We suggested switching to 42 HRC, adjusted their pre-drilled hole size, and the crack rate dropped to 0.2%. That’s the kind of thing that makes me love this job—helping folks get the right part, not just the hardest one.
Wait, also—how do we test insert hardness at our facility? For anyone curious, we use a portable Rockwell tester on every batch before shipping. No guessing, no cutting corners. Every insert we send out gets a quick hardness check to make sure it’s within that sweet spot we talk about. That’s why our customers come back—they know they’re getting consistent, reliable hardness, not a mix of duds and good parts like from some overseas suppliers.
Another myth I wanna bust: “self-tapping inserts are all the same hardness.” Nope. I’ve seen inserts from random suppliers that range from 25 HRC to 55 HRC, no consistency. One box could have inserts that are too soft, the next too hard. That’s why you need to buy from a supplier that knows what they’re doing, someone who doesn’t just grab cheap blanks from a factory and sell ‘em. We heat-treat our inserts in-house to get that exact hardness range, so every single one we send out is consistent.
Let’s wrap this up with what you should actually take away if you’re shopping for self-tapping inserts:
- Hardness is not strength—know your torque needs and load capacity too.
- Aim for that 10-15 HRC difference between your insert and base material to get clean threads.
- Don’t chase the highest HRC number—brittleness is a real problem.
- Consistency matters—ask your supplier for hardness test data on their batches, not just a spec sheet.

If you’re working on a project right now and you’re not sure what hardness insert you need, hit us up. We can walk you through your part material, torque specs, and application to hook you up with the perfect insert. No salesy pushy stuff—just real advice from someone who’s been in this game for years. Whether you need 100 inserts for a small prototype or 100,000 for a mass production run, we’ve got you covered. Just reach out to our team to start the conversation.
Key Locking Inserts References
ASM International. (2020). Hardness Testing Basics. Materials Park, OH: ASM International.
DIN Standard 7500-1. (2018). Self-tapping Inserts for Metal and Plastic Components. Berlin: German Institute for Standardization.
Kuhn, H. A. (2013). Metallurgy for the Non-Metallurgist (2nd ed.). Materials Park, OH: ASM International.
Locking Inserts Technologies Co., Ltd.
As one of the most professional self-tapping inserts manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to wholesale bulk self-tapping inserts in stock here from our factory. Also, custom service is available.
Address: 205, 2/F, Bldg. A8, Zhizaogu Ind. Park, No.26 Xingye 5th Rd, Bao’an Dist., Shenzhen, Guangdong, P.R.China
E-mail: sales@lockinginserts.com
WebSite: https://www.lockinginserts.com/
