As a header connector supplier with over 12 years in the electronic components industry, I’ve seen firsthand how rushed or careless termination processes can turn a seemingly standard header connector into a costly failure—whether that’s a prototype PCB that doesn’t pass testing, a mass-produced device that dies mid-assembly, or a field unit that returns with intermittent connectivity issues. Too often, teams treat termination as a last-minute afterthought: they grab a pair of scissors, strip a wire, and cram it into the connector pin, assuming the part is built to handle any rough handling. But here’s the hard truth: header connectors are precision parts, and their performance hinges entirely on how you terminate the mating component—whether that’s a wire, PCB trace, or ribbon cable. Header Connector
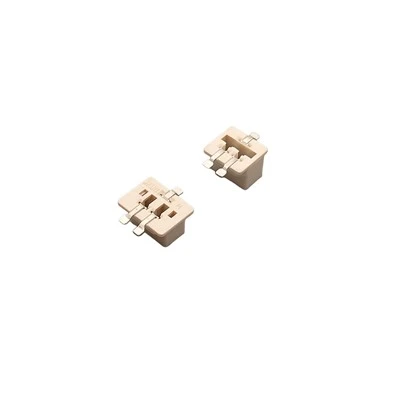
I remember a client call from 2019, when a medical device startup I’d been working with for months hit a wall. They were testing a portable glucose monitor, and 12% of their prototypes were failing functional tests because the power header connector wouldn’t maintain a consistent connection during drop tests. Their in-house technicians had been soldering wires directly to the header pins, but the thermal shock from the soldering iron was warping the thin copper plating on the pins, creating microscopic gaps that broke the current. It took us three days of troubleshooting to pinpoint the issue, and we fixed it only by teaching their team a standardized, low-heat termination method that preserved the connector’s internal structure. That experience stuck with me: good header connectors are only as good as the termination work that links them to the rest of the system.
This blog will walk you through the most common, reliable termination methods for header connectors, when to use each, and the mistakes to avoid—all from the perspective of a supplier who’s seen both successes and failures firsthand. Whether you’re a design engineer prototyping a new IoT sensor, a production manager scaling a consumer electronics line, or a technician troubleshooting a faulty field unit, these insights will help you get it right the first time.
First, let’s define what “termination” actually means for a header connector. For context, a header connector is a male pin or socket assembly that mounts to a PCB, intended to mate with a female connector, wire, or cable on the other side. Termination is the process of creating a permanent, low-resistance, mechanical bond between the connector’s pins and the mating component that will carry signals or power. There are four primary methods used today: crimping, soldering, insulation displacement contact (IDC) termination, and press-fit termination. Each has unique use cases, pros, and critical pitfalls that can ruin the connector’s performance.
Let’s start with the method I recommend most for low- to mid-volume applications: crimping. Crimping is the process of pressing a metal terminal (usually made of tin-plated copper, the standard for header connector mating) onto a stripped wire, creating a cold weld where the metal of the terminal and wire strands fuse under pressure. For header connectors, crimped terminals are the most common option because they’re fast, reliable, and resistant to vibration—critical for products like automotive sensors or industrial controls that move frequently.
Here’s how to do it correctly, step by step, from someone who’s trained dozens of technicians on this process. First, choose the right terminal for your wire gauge. Header connectors are rated for specific wire sizes, so always cross-reference the terminal’s AWG (American Wire Gauge) rating with your wire. Using a terminal that’s too small will crimp down on only a few wire strands, leaving loose strands that can break over time; a terminal that’s too large will have gaps that cause high resistance, leading to voltage drop or overheating. Next, strip the wire insulation to exactly the length specified by the terminal’s manufacturer. Most terminals have a strain relief barrel (the part that grips the insulation) and a wire barrel (the part that crimps to the copper strands). If you strip too much insulation, the wire will shift inside the terminal; too little, and the strain relief won’t hold, leading to pulled wires.
The biggest mistake I see with crimping is using the wrong crimping tool. Generic pliers won’t apply the uniform pressure needed to create a proper crimp—you need a hexagonal or quadrilateral crimp tool matched to your terminal type. I once had a client send back 5,000 crimped header connectors because their team used a basic pair of needle-nose pliers, resulting in 30% of the crimps having sharp edges that cut through the wire strands. A proper crimp should have a smooth, uniform shape, with no exposed copper between the terminal’s barrels. Also, always perform a pull test after crimping: a properly crimped wire shouldn’t pull free with 5 pounds of force, even for small 24AWG wires.
Next, soldering. Soldering is still widely used for header connectors, especially in high-volume PCB assemblies where the header is mounted directly to the board, or when mating to rigid PCBs instead of wires. Unlike crimping, soldering uses a molten metal alloy (usually tin-lead or lead-free, per RoHS standards) to bond the connector pin’s plating to the component (either a wire or PCB trace). It’s often seen as simpler than crimping, but it’s also the method most prone to failure if done incorrectly.
I’ve had clients ask why their soldered headers keep developing cold joints—those dull, grainy connections that don’t conduct electricity properly. The main issue here is heat management. Header connectors have thin, often gold-plated pins (for corrosion resistance), and too much heat from a soldering iron can burn through the gold plating, leaving only soft copper that oxidizes quickly, or warp the plastic housing of the header, causing pins to misalign. For through-hole headers, keep your iron temperature between 350°C and 375°C, and limit contact time to 2–3 seconds. For surface-mount headers, use a fine-tip iron and a controlled soldering station, not a handheld iron, to avoid overheating adjacent components.
Another common soldering mistake is not cleaning the pin or trace before soldering. Oil, flux residue, or oxidation on the pin will prevent the solder from bonding, leading to intermittent connections. Always use a small amount of no-clean flux (designed for electronic components) on the pin and trace before soldering, and ensure the solder forms a smooth, “bead” shape that covers the entire pin and trace, with no gaps. For wire-to-header soldering, avoid soldering directly to the plastic housing—keep the solder only on the metal pin, so the wire has enough flexibility to move without breaking the bond.
Third on the list is IDC termination, which is most often used for ribbon cables mating to header connectors. IDC stands for Insulation Displacement Contact, a technology where sharp edges on the connector’s pins cut through the wire’s insulation to make contact with the copper core—no stripping or soldering required. This is the fastest termination method for mass-produced products like computer motherboards or data acquisition systems, where hundreds of wires need to be terminated quickly.
The key to successful IDC termination is alignment and pressure. Ribbon cables are made of multiple parallel wires, and even a 0.5mm misalignment between the connector and the cable will cause a wire to miss the pin entirely, leading to open circuits. Always use an IDC crimping tool that’s matched to your ribbon cable pitch (common pitches are 1.27mm and 2.54mm, standard for header connectors). When inserting the cable into the connector, make sure the cable’s orientation matches the keyway on the connector—most IDC headers have a plastic notch that prevents reversed insertion, so double-check before applying pressure. A common failure point with IDC is insufficient crimp pressure: if the tool doesn’t apply enough force, the pins won’t cut through the insulation, leading to high resistance or no connection. I once worked with a server manufacturer that had a 8% failure rate in their data cables until they switched to hydraulic crimping tools for IDC termination; manual tools weren’t applying enough force to the 30AWG wires they were using.
The final method is press-fit termination, which is almost exclusively used for surface-mount or through-hole header connectors mounted directly to PCBs. Press-fit uses metal pins with a slight oversize diameter (usually 10–15% larger than the PCB’s drilled hole) to create a mechanical and electrical bond when pressed into the hole. This method eliminates the need for soldering, making it ideal for high-reliability applications like aerospace or military electronics, where vibration and thermal cycling can break soldered joints.
Press-fit termination requires precision in drilling and pin diameter. The PCB’s hole must be exactly the right size—too large, and the pin won’t make a consistent contact; too small, and you’ll damage the pin or the PCB’s copper plating during insertion. Always use a press-fit machine with controlled force, inserting the pins at a consistent speed (usually 1–2 mm per second) to avoid bending the pin or cracking the PCB. I’ve seen too many teams use a hand press for press-fit headers, resulting in crooked pins that don’t align with mating connectors, or partial insertion that leads to intermittent connections. For critical applications, use a gauge to verify the pin’s protrusion after insertion: it should be exactly 0.5mm above the PCB surface, enough to mate with the female connector without interfering.
Now, let’s talk about how to choose the right termination method for your project, because there’s no one-size-fits-all solution. If you’re prototyping a low-volume device (less than 1,000 units), crimping is your best bet—it’s flexible, easy to adjust if you change wire gauges, and has lower startup costs. For high-volume production (10,000+ units), IDC or press-fit will save you time and labor, even if the initial tooling cost is higher. For applications requiring ultra-reliability, like medical or aerospace, press-fit or cold crimping (not soldering) is non-negotiable, because soldered joints can degrade over time from thermal cycling.
I can’t stress this enough: never cut corners on termination. I’ve seen a $0.10 header connector fail a $10,000 field test because of a bad crimp, or a poorly soldered joint cause a product recall that cost a manufacturer $2 million. The header itself is a small part of the system, but it’s the critical link that keeps power and signals flowing. Even the highest-quality gold-plated header will fail if you terminate it with a mismatched tool, wrong material, or rushed process.

If you’re currently working on a project and running into issues with header connector termination—whether it’s intermittent connections, pull-off failures, or high resistance—I’m here to help. We supply a full line of header connectors compatible with all the termination methods I’ve outlined, and our team works directly with manufacturers to optimize termination processes for their specific applications. Whether you need custom crimp terminals, RoHS-compliant solder materials, or press-fit header assemblies, we can tailor a solution to your needs. Reach out to our team of component specialists to discuss your project, and let’s make sure your header connectors are terminated correctly, the first time.
Automotive Connector References
- “Termination Methods for Electronic Connectors.” International Electrotechnical Commission (IEC) Standard 60352-1, 2021.
- Crimp Termination: Best Practices for Reliable Connections. AIM Aerospace Components, 2020.
- Soldering Guidelines for Surface-Mount Header Connectors.IPC Association Standard J-STD-001, 2019.
- IDC Termination Performance for Ribbon Cables. TE Connectivity Application Note AN-007, 2022.
- Press-Fit Connector Design and Assembly. Society of Manufacturing Engineers (SME), 2021.
Wenzhou JKUN Connector Co., Ltd.
As one of the most professional header connector manufacturers and suppliers in China, we’re featured by quality products and low price. Please rest assured to wholesale bulk customized header connector from our factory. For quotation and free sample, contact us now.
Address: No.2667, Ningkang East Road, Yueqing City, Zhejiang Province, China
E-mail: sales@cnjkun.com
WebSite: https://www.jkunjcj.com/
